Phone:
+85295718875
Email:
support@just-wonders.com
Phone:
+85295718875
Email:
support@just-wonders.com
Learn what a pre-shipment inspection can verify, how sampling changes the result, and when to release, correct, or re-inspect a supplier lot.
A supplier can tell you that an order is finished, but “finished” is not the same as ready to ship. A pre-shipment inspection (PSI) is the last practical checkpoint for comparing a production lot with the specification you approved, before defects become freight, rework, returns, and customer-service work. It is most useful when the order is substantially complete and there is still time to correct a problem.
This guide explains what a pre-shipment inspection can verify, how to write a useful inspection checklist, how sampling changes what a result means, and what you should do with the report. The key decision is not simply pass or fail: it is whether the evidence is strong enough to release this lot, request correction, or hold shipment while the supplier fixes a defined issue.
QIMA describes a pre-shipment inspection as an on-location review when at least 80% of an order is complete and packing has begun. That timing matters. If an inspector arrives while too little product exists, the sample may not represent the finished lot. If the inspection waits until every carton is sealed and the truck is booked, a failed finding can turn into an expensive delay rather than a manageable correction.
Give the inspector, your purchasing team, or your warehouse a single version of the approved specification before the visit. Include the purchase order, approved sample, drawings or measurements, colour references, artwork, labels, accessory list, packaging instructions, and the destination requirements that actually apply. A pre-shipment inspection cannot repair an unclear brief. It can only compare observable goods with the criteria you supplied.
Before booking, define the lot. State the supplier, purchase-order number, SKU or style, colour and size breakdown, planned quantity, production location, and the portion that is complete. If several colours or variants are packed together, keep the counts separate. A total that hides one missing variant can look acceptable while a customer-facing assortment is still incomplete.
A useful supplier quality inspection checklist says what will be looked at, how it will be compared, and what evidence will be recorded. “Good quality” is too vague to guide a release decision. Translate it into observable checks that a second person could repeat without guessing.
Product identity and quantity. Count finished, semi-finished, and packed units separately. Match the SKU, colour, size, model, and assortment to the order. Record shortages, substitutions, mixed cartons, and units that are still in production. For a kit or bundle, check the components together; a complete count of the main item does not prove that every accessory is present.
Appearance and workmanship. Define the defects that matter to a buyer: stains, scratches, open seams, loose threads, crooked attachments, uneven printing, damaged hardware, poor assembly, or visible variation between units. Photograph a defect beside a reference or measurement when possible. The purpose is not to collect alarming pictures; it is to make the finding unambiguous enough for a supplier to correct.
Dimensions, materials, and function. List the dimensions that affect fit or use, the material or component that was approved, and any simple function test that a unit must pass. A pouch may need its zipper to open and close; a device may need its buttons to respond; a folded textile may need the correct label and construction. If a requirement needs laboratory equipment or a regulated test, mark it as a separate verification instead of pretending a visual inspection proves it.
Artwork, labels, and compliance information. Compare spelling, font, placement, size, care or warning labels, and required marks against the approved artwork. Check that the label belongs to the correct variant. A visually attractive product with the wrong instruction label is still a release problem.
Packing and shipping marks. Verify inner and outer packing, protective material, carton dimensions, carton weight, quantities per carton, and shipping marks. These details help a freight partner plan the shipment and reduce repacking or customs questions. They also create a useful bridge between the inspection record and the warehouse receiving record.
Most pre-shipment inspection is an acceptance-sampling exercise, not a promise that every unit was opened and tested. QIMA’s pre-shipment inspection description says its inspectors randomly select samples using ANSI/ASQ Z1.4-2008. The NIST/SEMATECH e-Handbook’s acceptance-sampling overview explains how sample information is used to make a decision about a production lot. Together, those references support treating the sample as a defined decision rule rather than as proof that every unit was tested.
Those standards help structure a sample; they do not choose your product requirements for you. Agree the lot definition, inspection level, critical/major/minor defect categories, and acceptance numbers with the party responsible for quality before the inspection starts. Do not copy an AQL number from a random template and call it a safety limit. A sampling plan is a decision rule for the inspected lot, not a guarantee that no uninspected unit contains a defect.
Ask the inspector to record how units were selected and how many were checked. If a sample is drawn only from the easiest cartons to reach, or only from one colour, the report can look precise while its coverage is weak. For mixed lots, the sample should reflect the variants that the release decision covers. When a serious defect appears, preserve the actual unit, location, SKU, and photographs so the supplier can trace the cause instead of arguing over a vague percentage.
Sampling also affects how you describe the result to customers. “The inspected sample met the agreed acceptance plan” is accurate. “Every unit is perfect” is not. Keep the wording in your internal record and product claims aligned with the evidence you actually collected.
A clear defect report should connect each finding to a requirement, a location, a count, a severity, and a correction. Ask for a short summary that separates critical, major, and minor findings, but keep your own definitions visible. A broken safety feature and a slightly uneven fold should not be merged into one undifferentiated score.
If the result passes, reconcile the inspected quantity with the packing list and keep the report with the purchase record. If it is conditional, write the exact release conditions: for example, replace a defined number of damaged units, correct one label file, or re-pack a specified carton range. A conditional decision without an owner and a deadline is only a note, not control.
If the inspection fails, hold the shipment and send the supplier the evidence-backed correction list. Ask what was reworked, how many units were affected, and whether the lot was mixed with new production. Then arrange a re-inspection or a focused verification that matches the original failure. Do not silently average a failed sample with a later good sample; preserve both reports and explain what changed.
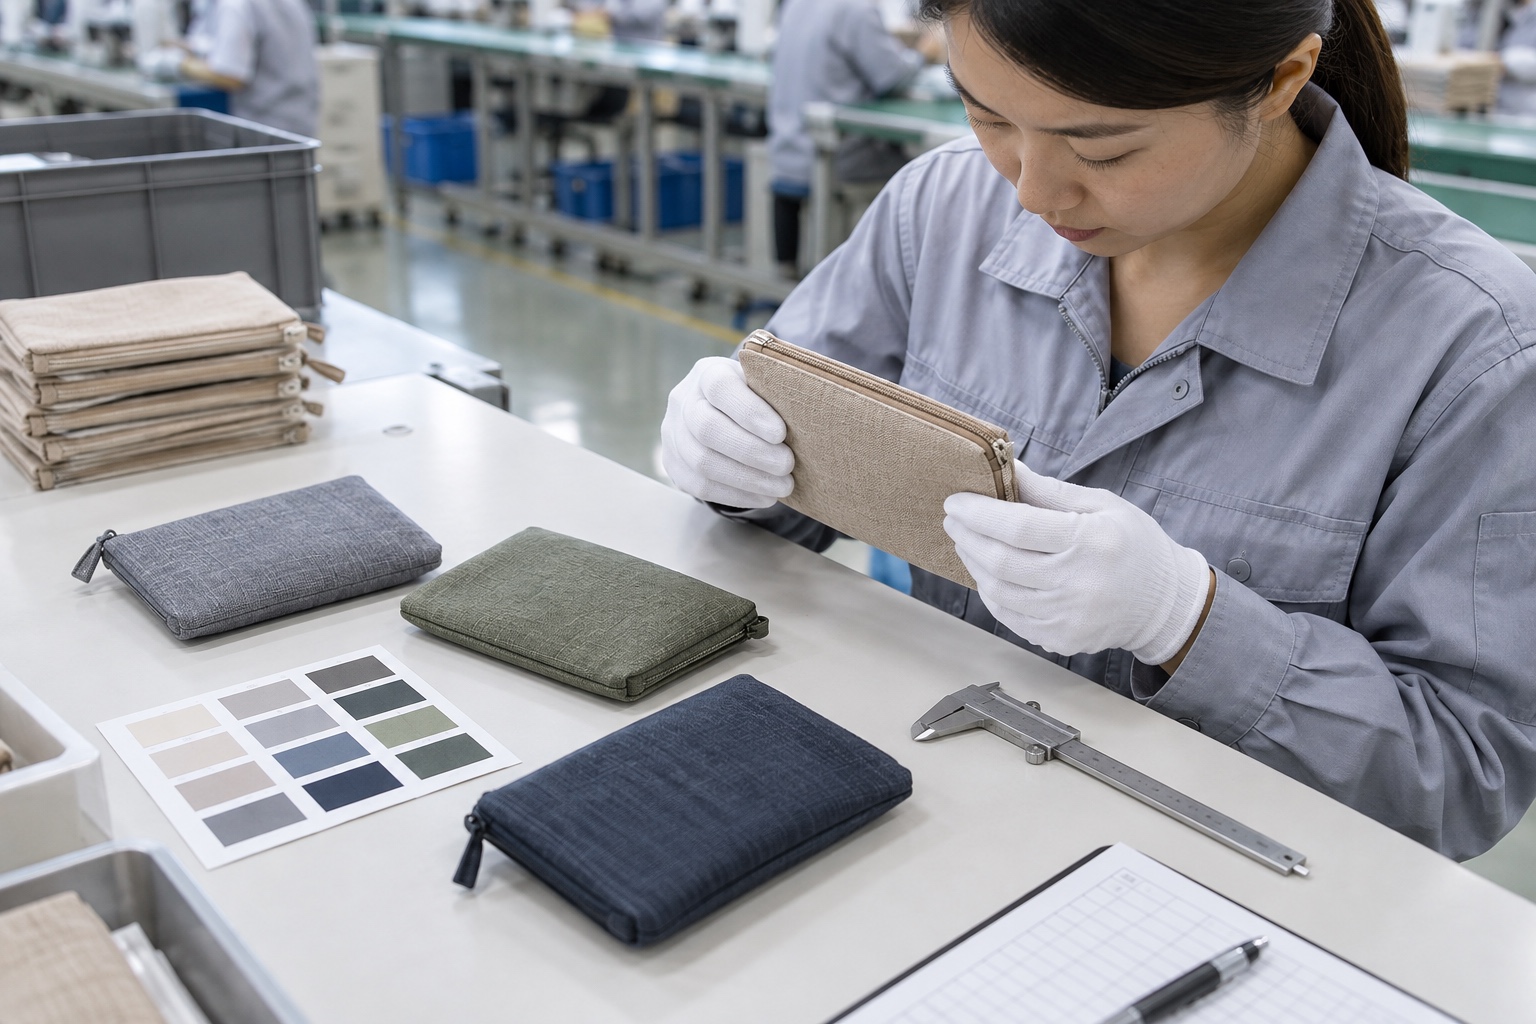
For repeat suppliers, track defect patterns by SKU, process, and shipment. A recurring crooked label points to artwork control or a fixture; repeated carton shortages point to packing or counting; a function failure may need a process or component change. The value of a pre-shipment inspection grows when each report improves the next specification instead of disappearing in an inbox.
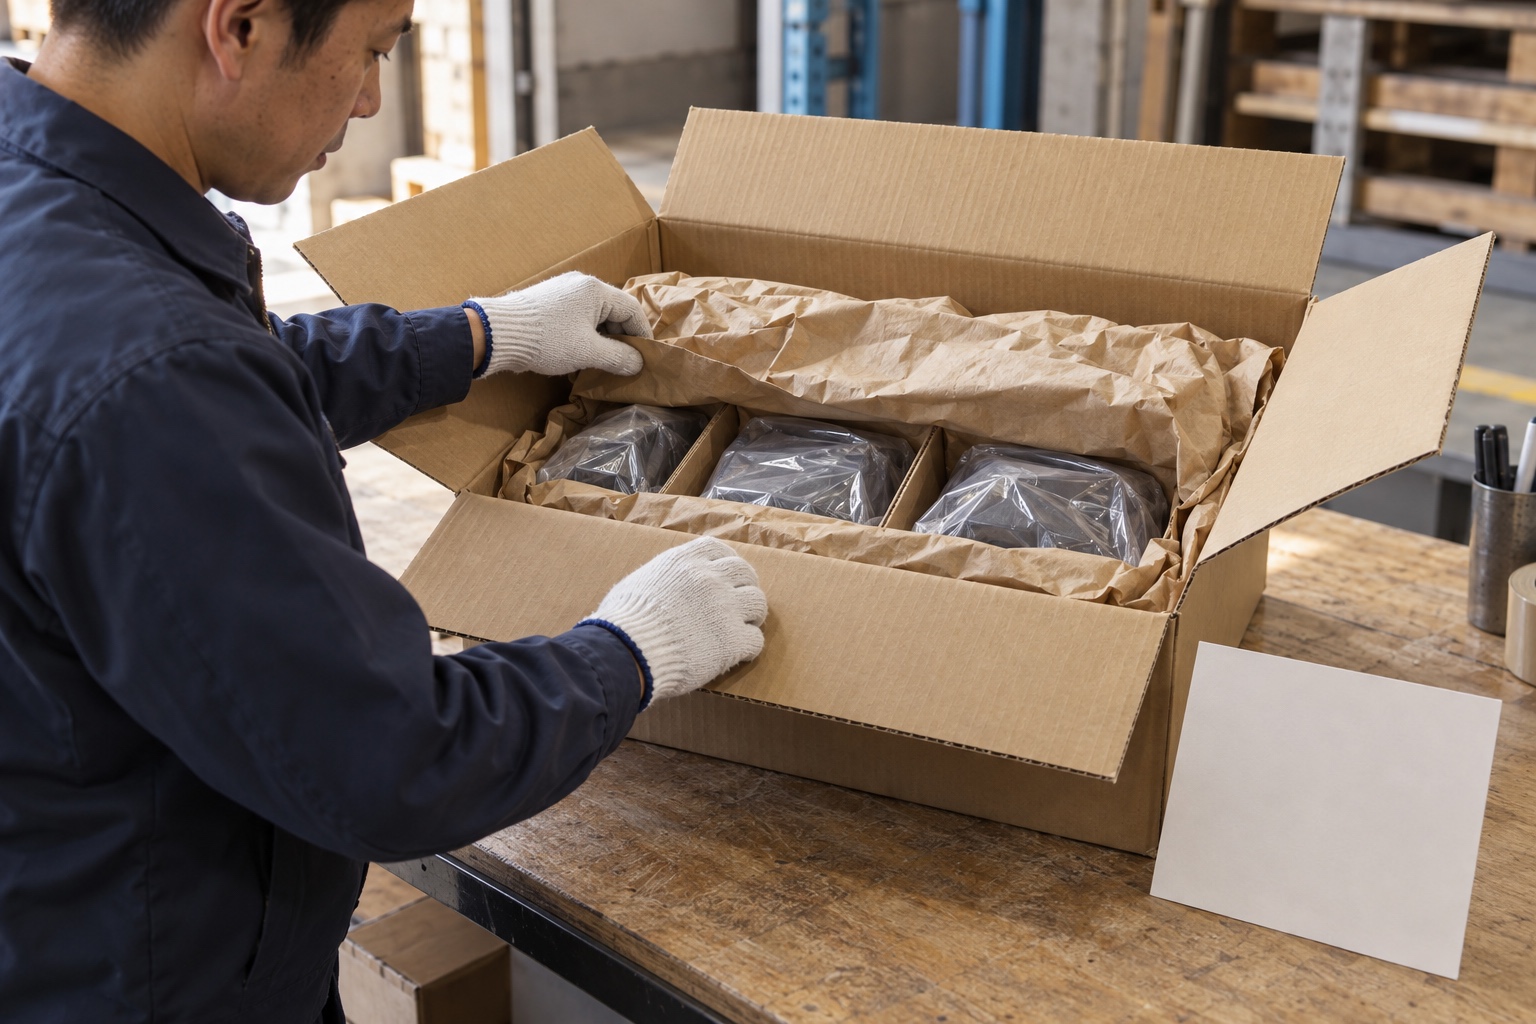
A pre-shipment inspection is a checkpoint, not a substitute for every other form of assurance. A visual and functional sample does not establish chemical compliance, electrical safety, long-term durability, or performance under every transport condition. QIMA explicitly notes that product testing may need to be combined with PSI when a product requires compliance testing. Keep laboratory reports, certificates, and transport tests as separate evidence with their own scope and dates.
Nor does a pass transfer responsibility for a vague specification to the inspector. If a colour reference, dimension tolerance, packaging strength, or accessory list was never agreed, the report cannot invent one after the fact. For a new product, approve a representative sample and make the important differences measurable before mass production starts.
The report also does not replace receiving control. Cartons can be damaged after the inspection, quantities can change during loading, and the wrong shipment can be dispatched. Match the inspection record to the final packing list and repeat the essential count when goods reach the warehouse. This is where a documented pre-shipment inspection connects to UploadToSell’s receiving and inspection workflow, rather than pretending that one visit covers the entire logistics chain.
Before approving dispatch, keep five items together: the approved specification, the lot and sample definition, the completed checklist, the defect photographs and corrections, and the final release decision. Add the carton count, dimensions, weights, and shipping marks that your forwarder will use. If the order requires supplier negotiation or consolidation, UploadToSell’s purchasing service can keep those records with the quote and purchase trail; do not present that service link as proof that a third-party PSI was performed.
A practical release question is: “What evidence would make me comfortable sending this lot to a customer?” If the answer is a corrected label, a rechecked carton, a passed function test, or a clean re-inspection, write that requirement before anyone books freight. The inspection then becomes a decision gate rather than a decorative report.
Start with the risk that matters most for the product and the customer promise. Define it, sample it fairly, record defects precisely, and keep the limits of the inspection visible. That discipline will not make an imperfect supply chain disappear, but it gives you time to correct preventable problems before they travel.
When should a pre-shipment inspection happen? Schedule it when most of the order is complete and packing has begun, while there is still time for corrective work. QIMA describes 80% completion as its usual timing; your production plan may require a different practical threshold.
Does a pre-shipment inspection check every item? Usually it uses an agreed sample. The report should state the lot, method, sample size, defects found, and acceptance rule. It should not be rewritten as a 100% guarantee.
What if the sample fails? Hold release, send the supplier the specific findings, verify the correction, and arrange a re-inspection or focused check. Keep the original failure and the later result linked so the decision history remains clear.